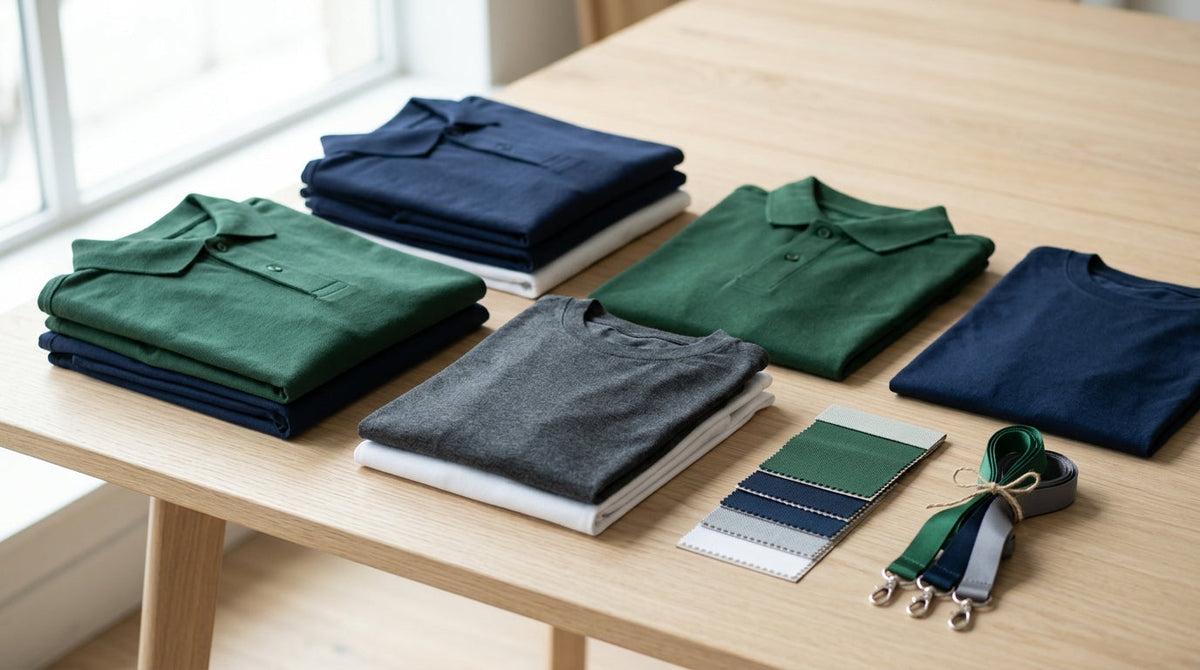

From corporate team-building polo shirts and retail staff uniforms to promotional run tees and conference crews, apparel branding directly shapes how your organization is perceived in public. Choosing between DTF (Direct-to-Film) transfers, multi-head embroidery, screen printing, and heat-transfer sublimation depends on fabric weave, artwork colour complexity, and wash-cycle frequency.
1. DTF (Direct-to-Film) Printing: Full-Colour Detail Without Heavy Setup Barriers
When artwork includes gradients, photorealistic badges, fine typography, or multi-colour chest and back prints on both light and dark cotton/blend garments, DTF (Direct-to-Film) printing excels. Printed onto specialized PET transfer film with elastic white under-base ink and hot-melt adhesive powder, DTF bonds cleanly onto cotton tees, hoodies, caps, and tote bags with strong wash elasticity and soft hand feel.
2. Corporate Machine Embroidery: Executive Authority on Pique Polos & Caps
For customer-facing uniforms, hospitality jackets, executive pique polo collars, and field staff caps, stitched thread remains the gold standard of longevity. Digitized corporate embroidery & fabric branding converts crisp vector crests into dense stitch files tailored to GSM weight, preventing puckering on woven oxfords and heavyweight polos across repeated industrial laundering.
3. Screen Printing & Sublimation: High-Volume Tees & Sportswear
For simple 1-to-3 spot colour event t-shirts in large batches, silk screen printing delivers clean ink opacity and crisp Pantone spot matching. Conversely, when producing marathon jerseys, dry-fit activewear, or all-over colour polyester pieces that must remain 100% breathable with zero ink build-up, heat-transfer sublimation printing infuses dye directly into light polyester fibers.


4. Side-by-Side Comparison: Choosing the Right Textile Branding Process
| Method | Ideal Fabric Substrates | Artwork & Finish Strengths | Best Use Case |
|---|---|---|---|
| DTF Printing | Cotton, poly-cotton, canvas totes, dark/light garments | Unlimited colours, photographic shading, clean thin text | Multi-colour company tees, staff kits, promos |
| Machine Embroidery | Pique polos, oxford shirts, jackets, twill caps | Raised premium thread texture, unmatched wash life | Corporate uniforms, reception teams, caps |
| Screen Printing | Cotton tees, hoodies, flat fabric panels | Solid Pantone ink vibrancy on bold spot designs | Large corporate retreats, roadshow merch |
| Sublimation | White/light polyester & dry-fit sportswear | Zero-feel breathability, cracks impossible | Corporate runs, sports teams, activewear |
5. Finishing Touches & Submitting an Apparel Branding Brief
Complete uniform and event rollouts with branded kraft garment swing tags and event wristbands, or browse all garment customization capabilities in our apparel & textile branding collection and printing services hub. Send your garment type, colour mix, placement positions, and vector artwork via the custom print quote page to receive confirmed pricing and scheduling for your batch.


Leave a comment
This site is protected by hCaptcha and the hCaptcha Privacy Policy and Terms of Service apply.